Send us a text

Text with us!

By submitting this form, you agree to our Terms of Service & Privacy Policy.

Stainless sanitary pipeline welded in a rotary dairy parlor
Sanitary welding · Monmouth, OR · Willamette Valley

Sanitary welds that pass inspection.

Tested, certified sanitary TIG work on 304 and 316L stainless product lines: dairy pipelines and bulk tanks, brewhouse and cellar fittings, winery tank work, distillery lines and food-grade equipment. Based in Monmouth, mobile across the Willamette Valley.

5.0
Google rating, 16 reviews★★★★★
USMCVeteran owned. Marine Corps, then a decade of Oregon welding.
24/7After-hours and emergency calls for lines that cannot wait.
  • Who we weld for
  • Dairies
  • Breweries
  • Wineries
  • Distilleries
  • Food processors
  • Commercial kitchens
Tested and certifiedSanitary welding is a separate test. Caleb took it and passed it.
Argon back-purgedEvery product-contact joint, full penetration, root as clean as the cap.
Left ready for the borescopeWelds stay unpolished until your inspector has seen them.
Mobile, on your siteParlor, milk room, brewhouse or cellar. Shop work in Monmouth for spools and manifolds.
Why sanitary is its own trade

A weld that would pass anywhere else can dump a tank of milk.

Inside a product line, the weld is a surface your milk, wort, wine or spirit touches on every run. Any pit, skip, crevice or oxidized root is a pocket where residue sits and bacteria grow through a clean-in-place cycle. On a Grade A dairy, the inspector who finds one can fail the line, and the tank it fed gets dumped. Some dairies in this valley run 10,000-gallon bulk tanks. In a brewery or winery the same flaw shows up as an infection you cannot trace and a batch you cannot sell.

That is why sanitary welding is tested separately, why few welders ever take the test, and why the ones who pass it charge for the extra care it takes. Caleb has done this work on working dairies and a distillery, and the dairy inspectors in this part of the valley know his work.

“If there is anything in that weld, an inspector on a dairy or a brewery will fail it and you redo it. It has to be perfect.”

Caleb Erickson, owner
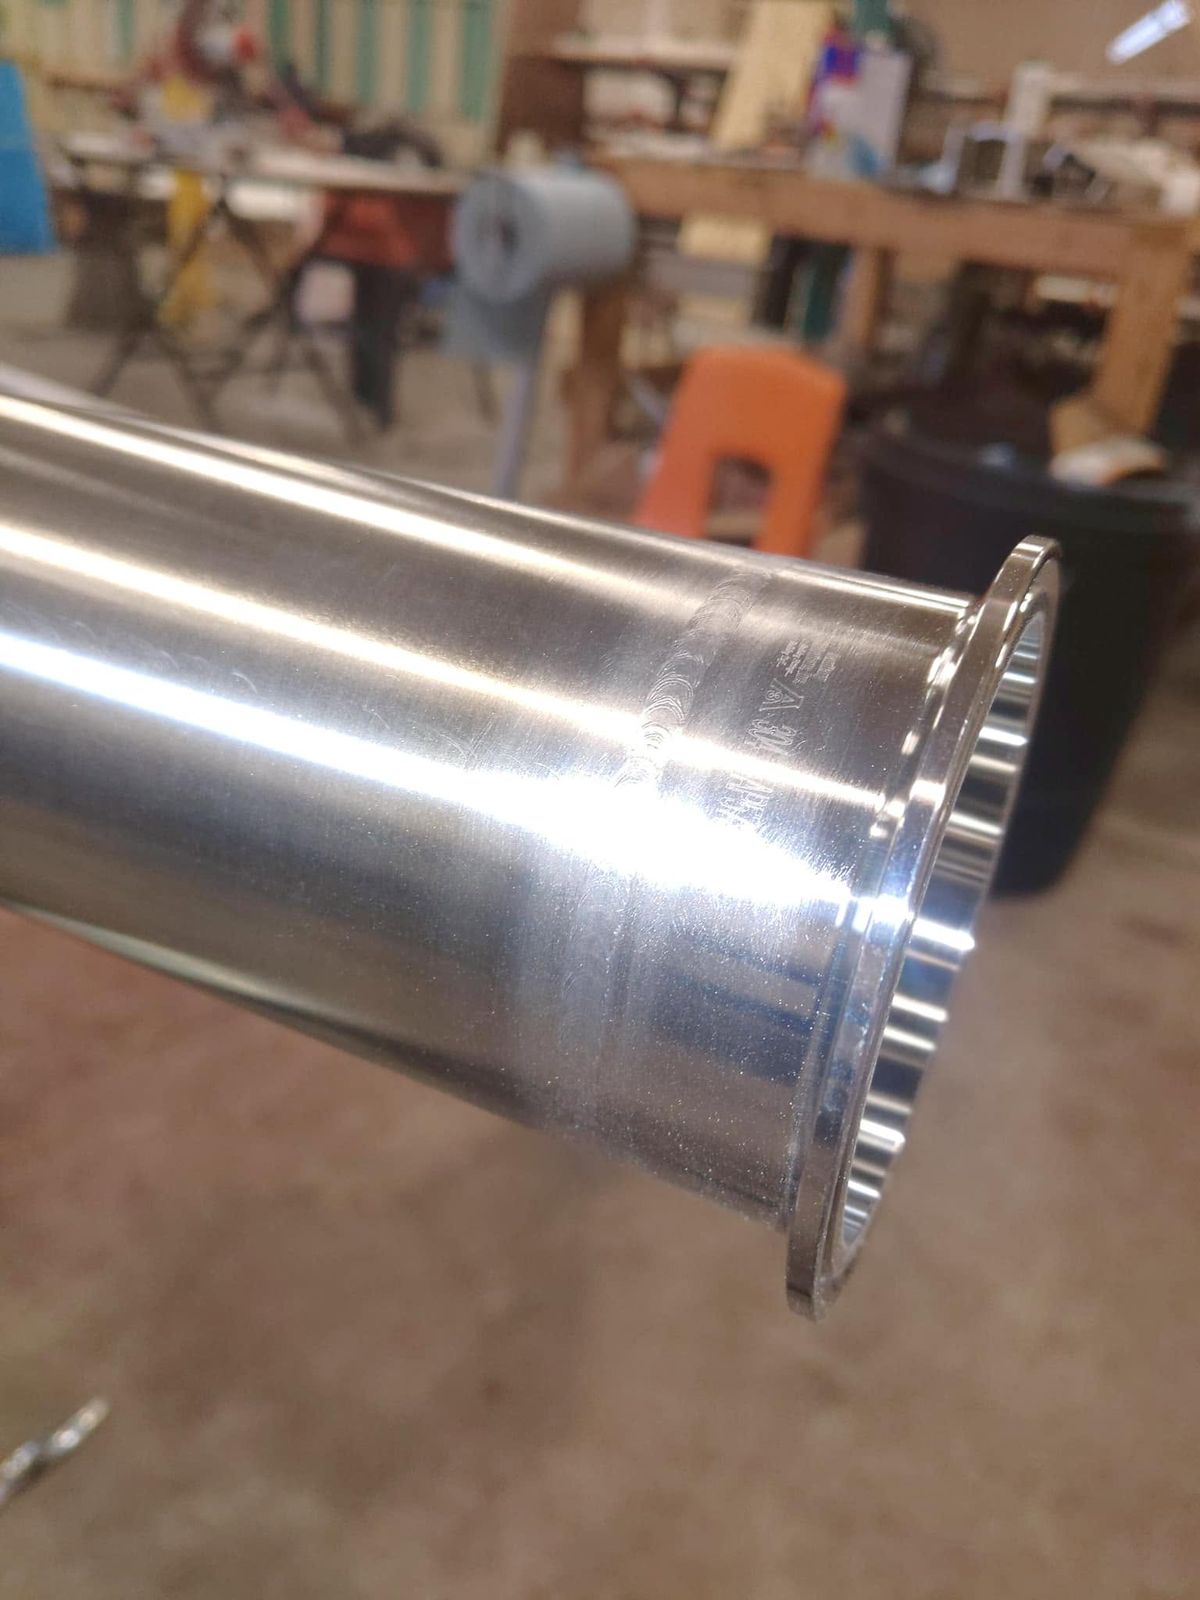
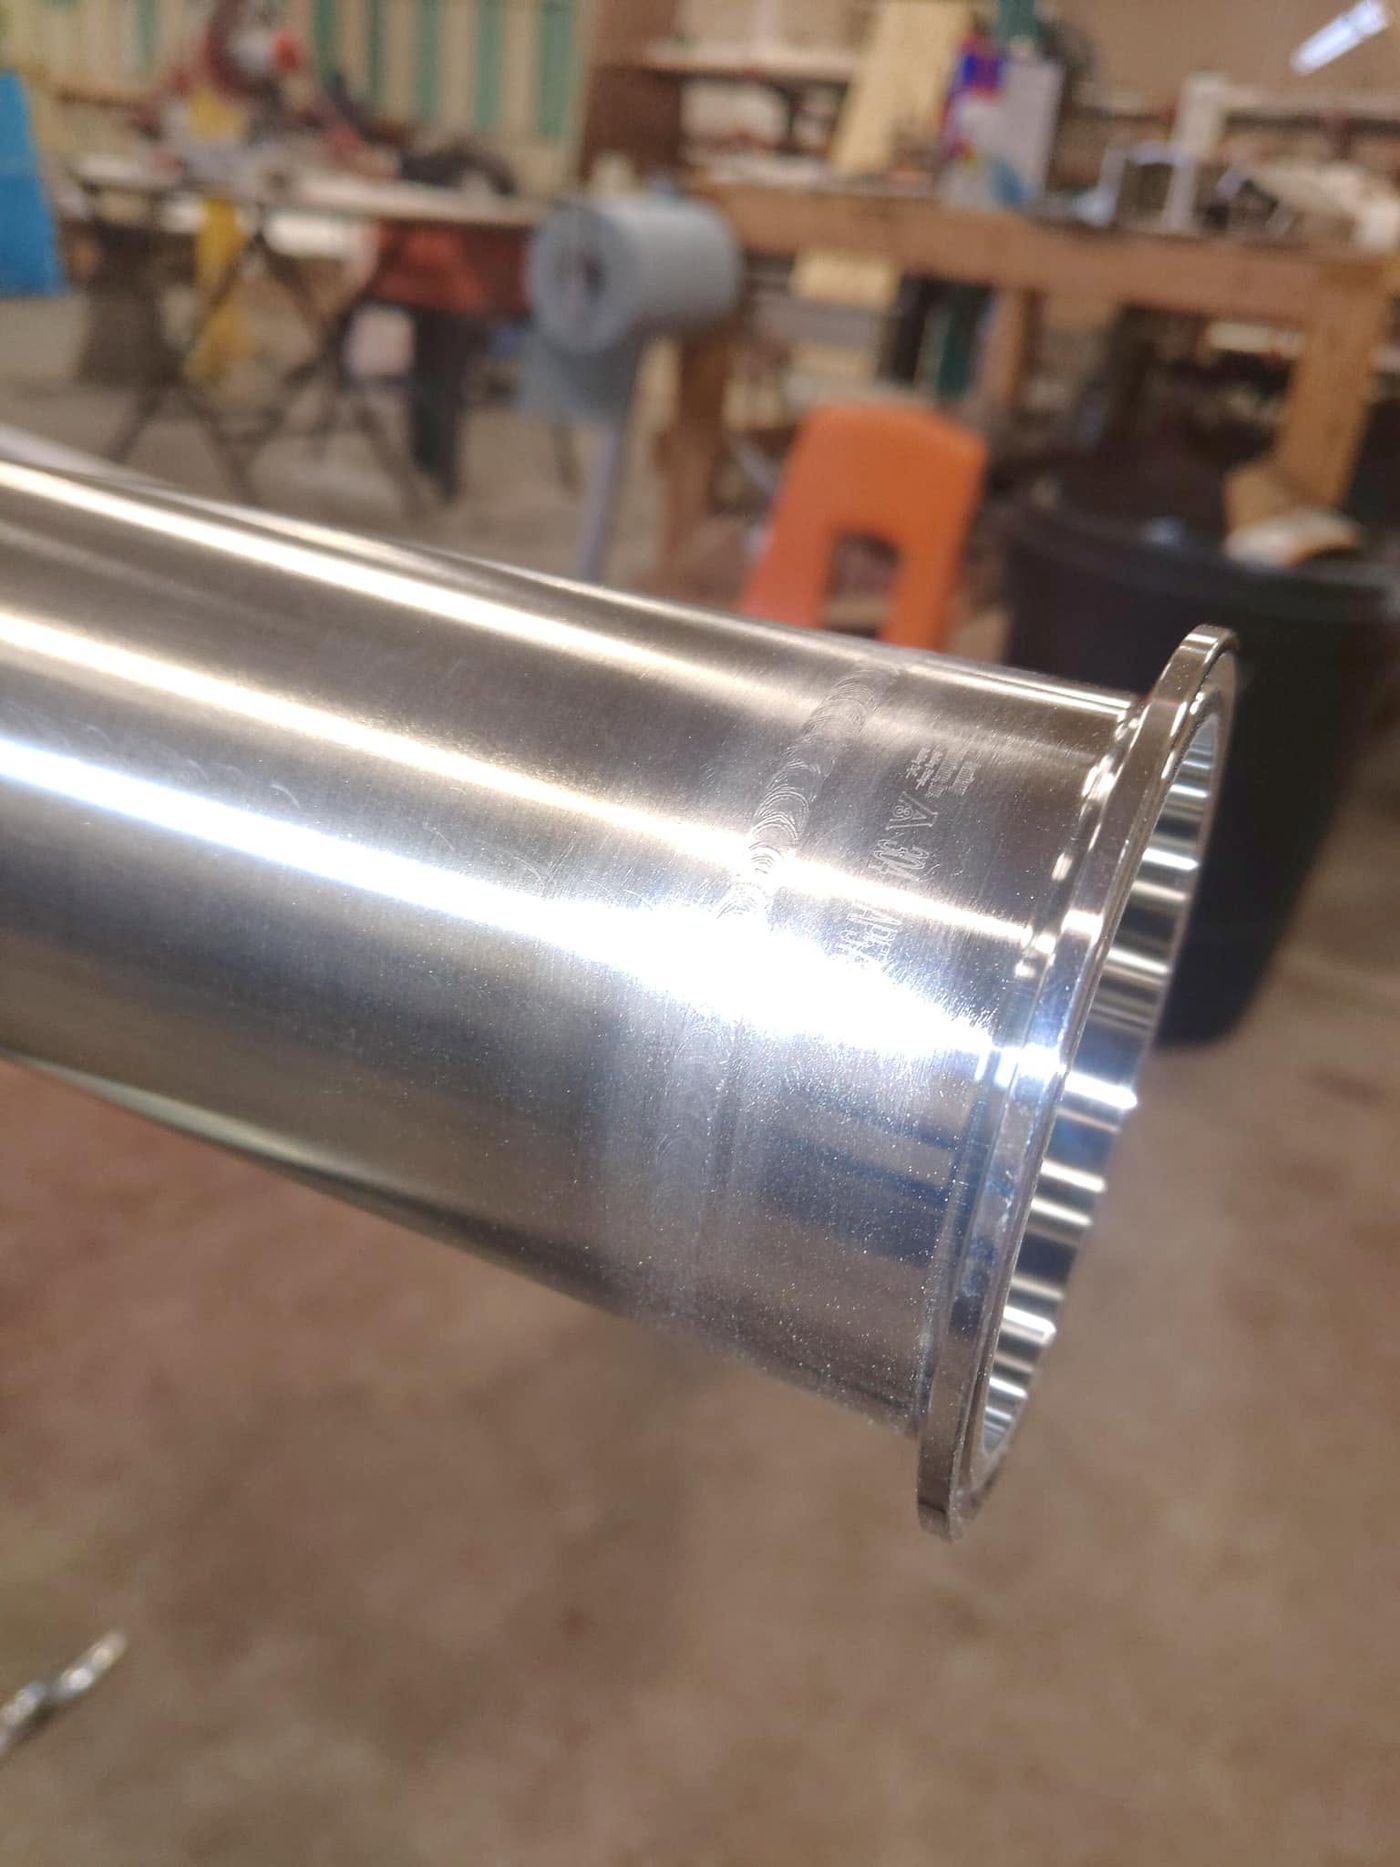
Tri-Clamp ferrule welded to sanitary stainless tube, weld left unpolished for inspection
Ferrule to tube. Unpolished so the inspector sees the weld, not the buff.
What the inspector looks for

Six ways a sanitary weld fails. How ours are built not to.

The acceptance criteria for a field-welded product line come down to three things: the joint is sound, it is smooth enough to clean, and the line drains. These are the flaws that break those rules, and what we do about each one.

FlawWhy it failsWhat we do
Sugared root
Why it fails
No back purge, or a purge that quit early. Oxygen hits the inside of the joint and the root comes out gray and grainy, like burnt sugar. It traps residue and it rusts.
What we do
Every product-contact joint is argon back-purged, and the purge stays on until the root is as bright as the cap. No exceptions for “just one quick fitting.”
Pits, skips, no penetration
Why it fails
A weld that did not fuse all the way through leaves a ledge or a crater on the inside where product collects. From the outside it can look fine.
What we do
Full-penetration passes at controlled heat. Any joint with a pit, crater, ridge or embedded material gets cut out and rewelded, the way 3-A practice calls for.
Heavy heat tint
Why it fails
Dark blue, purple or burnt discoloration means too much heat and a damaged chromium layer. It corrodes first and cleans worst.
What we do
Heat input kept low so tint stays in the light-straw range. Discoloration judged against the AWS D18.2 color levels, and reworked when it is over the line your plant allows.
Crevices at the joint
Why it fails
Tube ends that are out of round, off-square or misaligned leave a step inside the line. Product catches on the step, CIP flow skips over it.
What we do
Ends cut square, deburred and fit flush. Inside diameters matched so there is nothing to catch on, then checked again before the arc strikes.
Carbon contamination
Why it fails
A wire brush or flap disc that touched mild steel leaves iron in the stainless. It shows up later as rust spots on a line that was never supposed to rust.
What we do
Stainless-only brushes, discs and tooling that never touch carbon steel. Clean filler, clean gloves, clean tube.
Lines that will not drain
Why it fails
A run that sags or pitches the wrong way holds solution after CIP. Standing liquid is where growth starts.
What we do
Lines pitched to drain points and supported so they stay that way. Checked with a level, the same way the inspector will check it.
3-A3-A Sanitary Standards and Accepted Practice 605 for welded product pipelines and CIP systems in dairy and food plants: inert back-up gas, complete penetration, drainable lines, welds inspected before polishing.
AWS D18.1The welding specification for austenitic stainless tube and pipe in sanitary (hygienic) service, written with 3-A. Its companion D18.2 is the color guide for acceptable discoloration inside the tube.
304 / 316LSanitary tube and Tri-Clamp ferrules, elbows, tees and valves in the alloy that matches what you have. 316L where acid, salt or chlorides are in play.
Who it is for

Anywhere a product touches stainless.

Most of this work is dairies and the beverage side of the Willamette Valley. If your plant has a sanitary line, a tank or a piece of stainless equipment that an inspector or a brewer will judge, it belongs here.

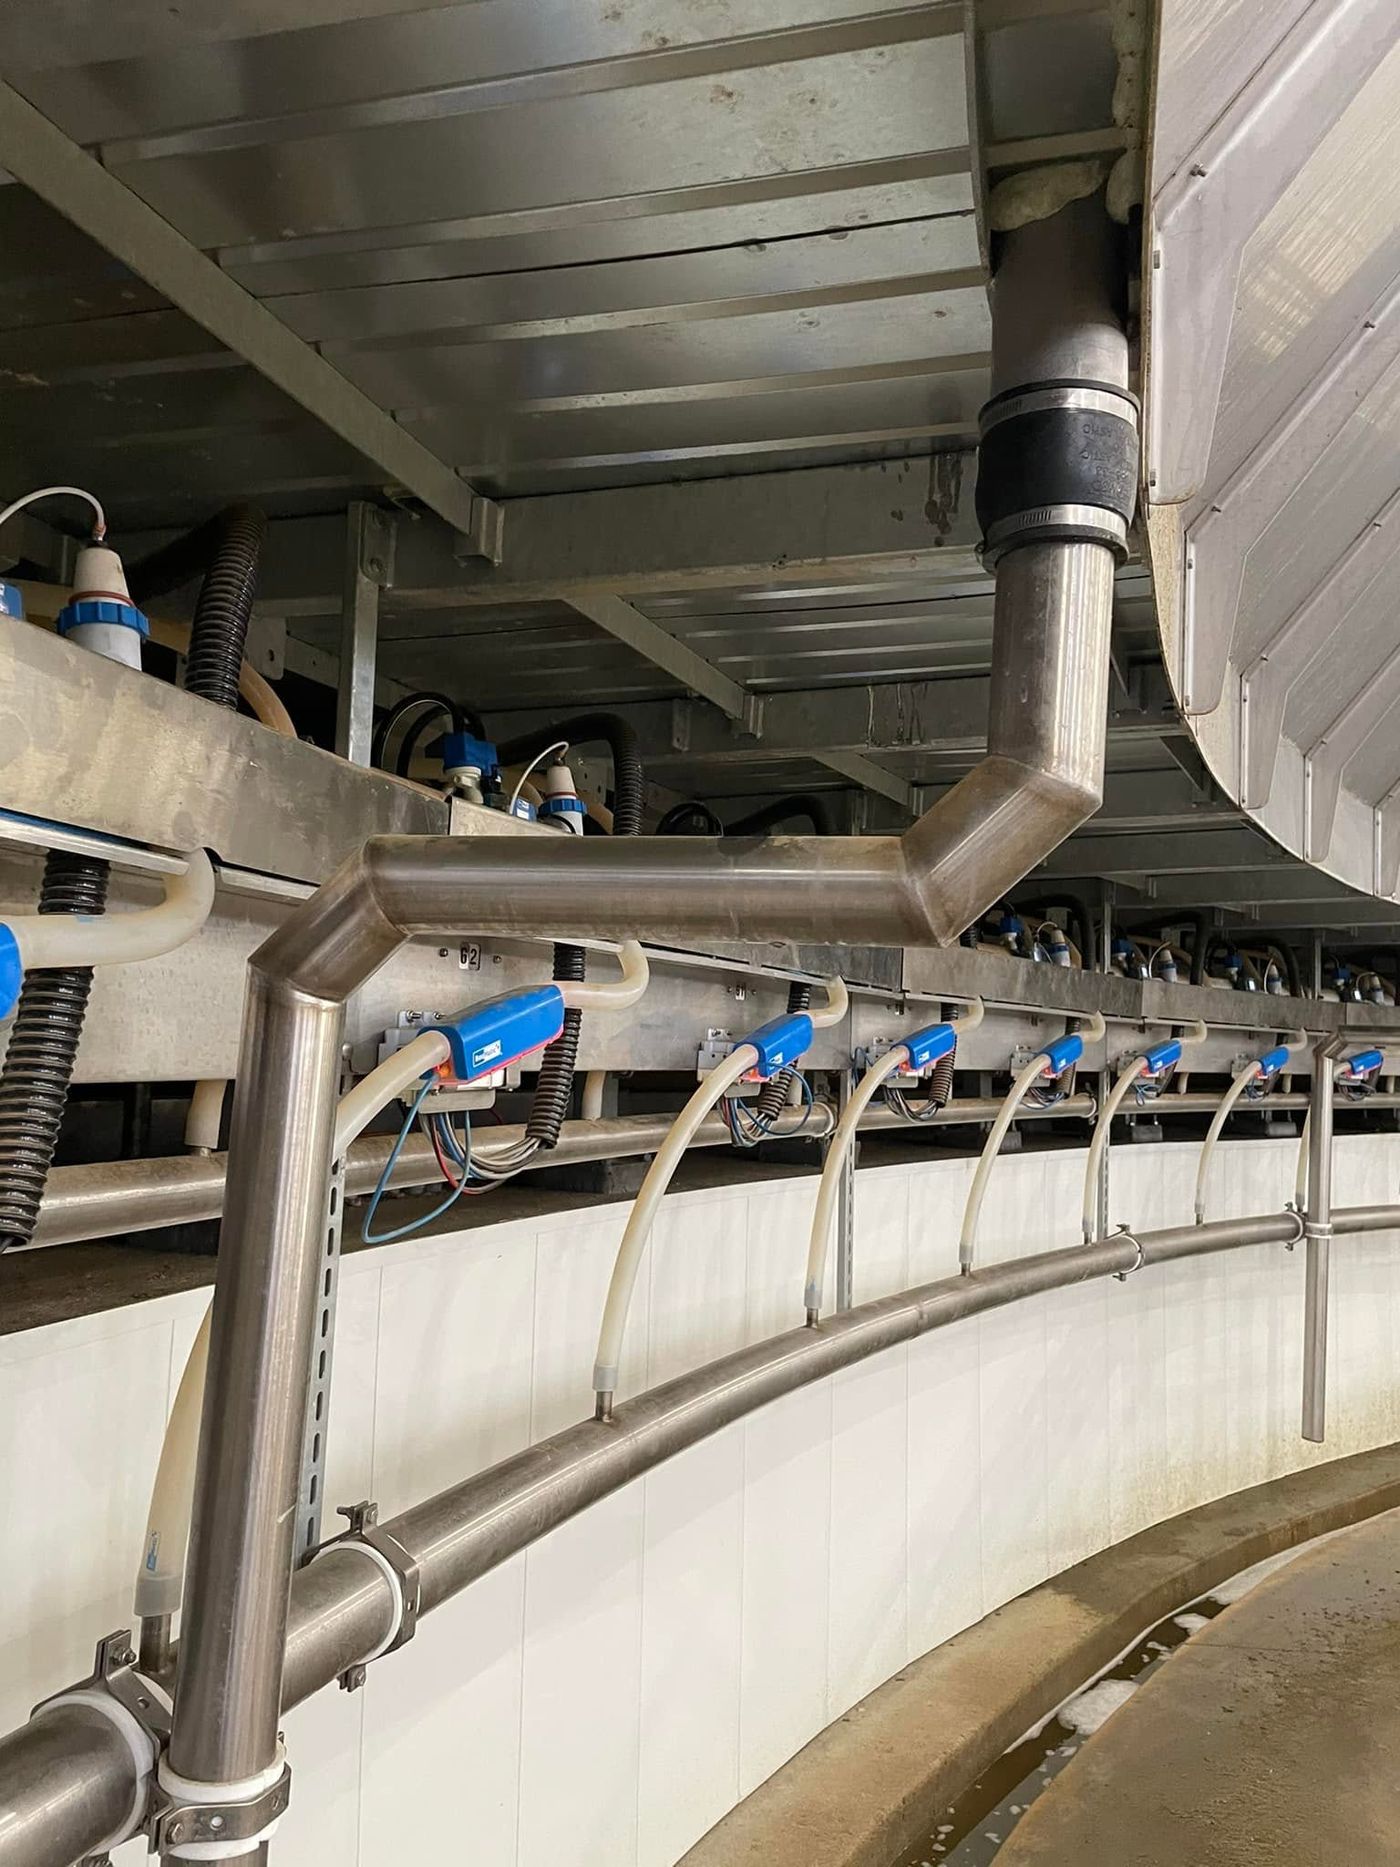
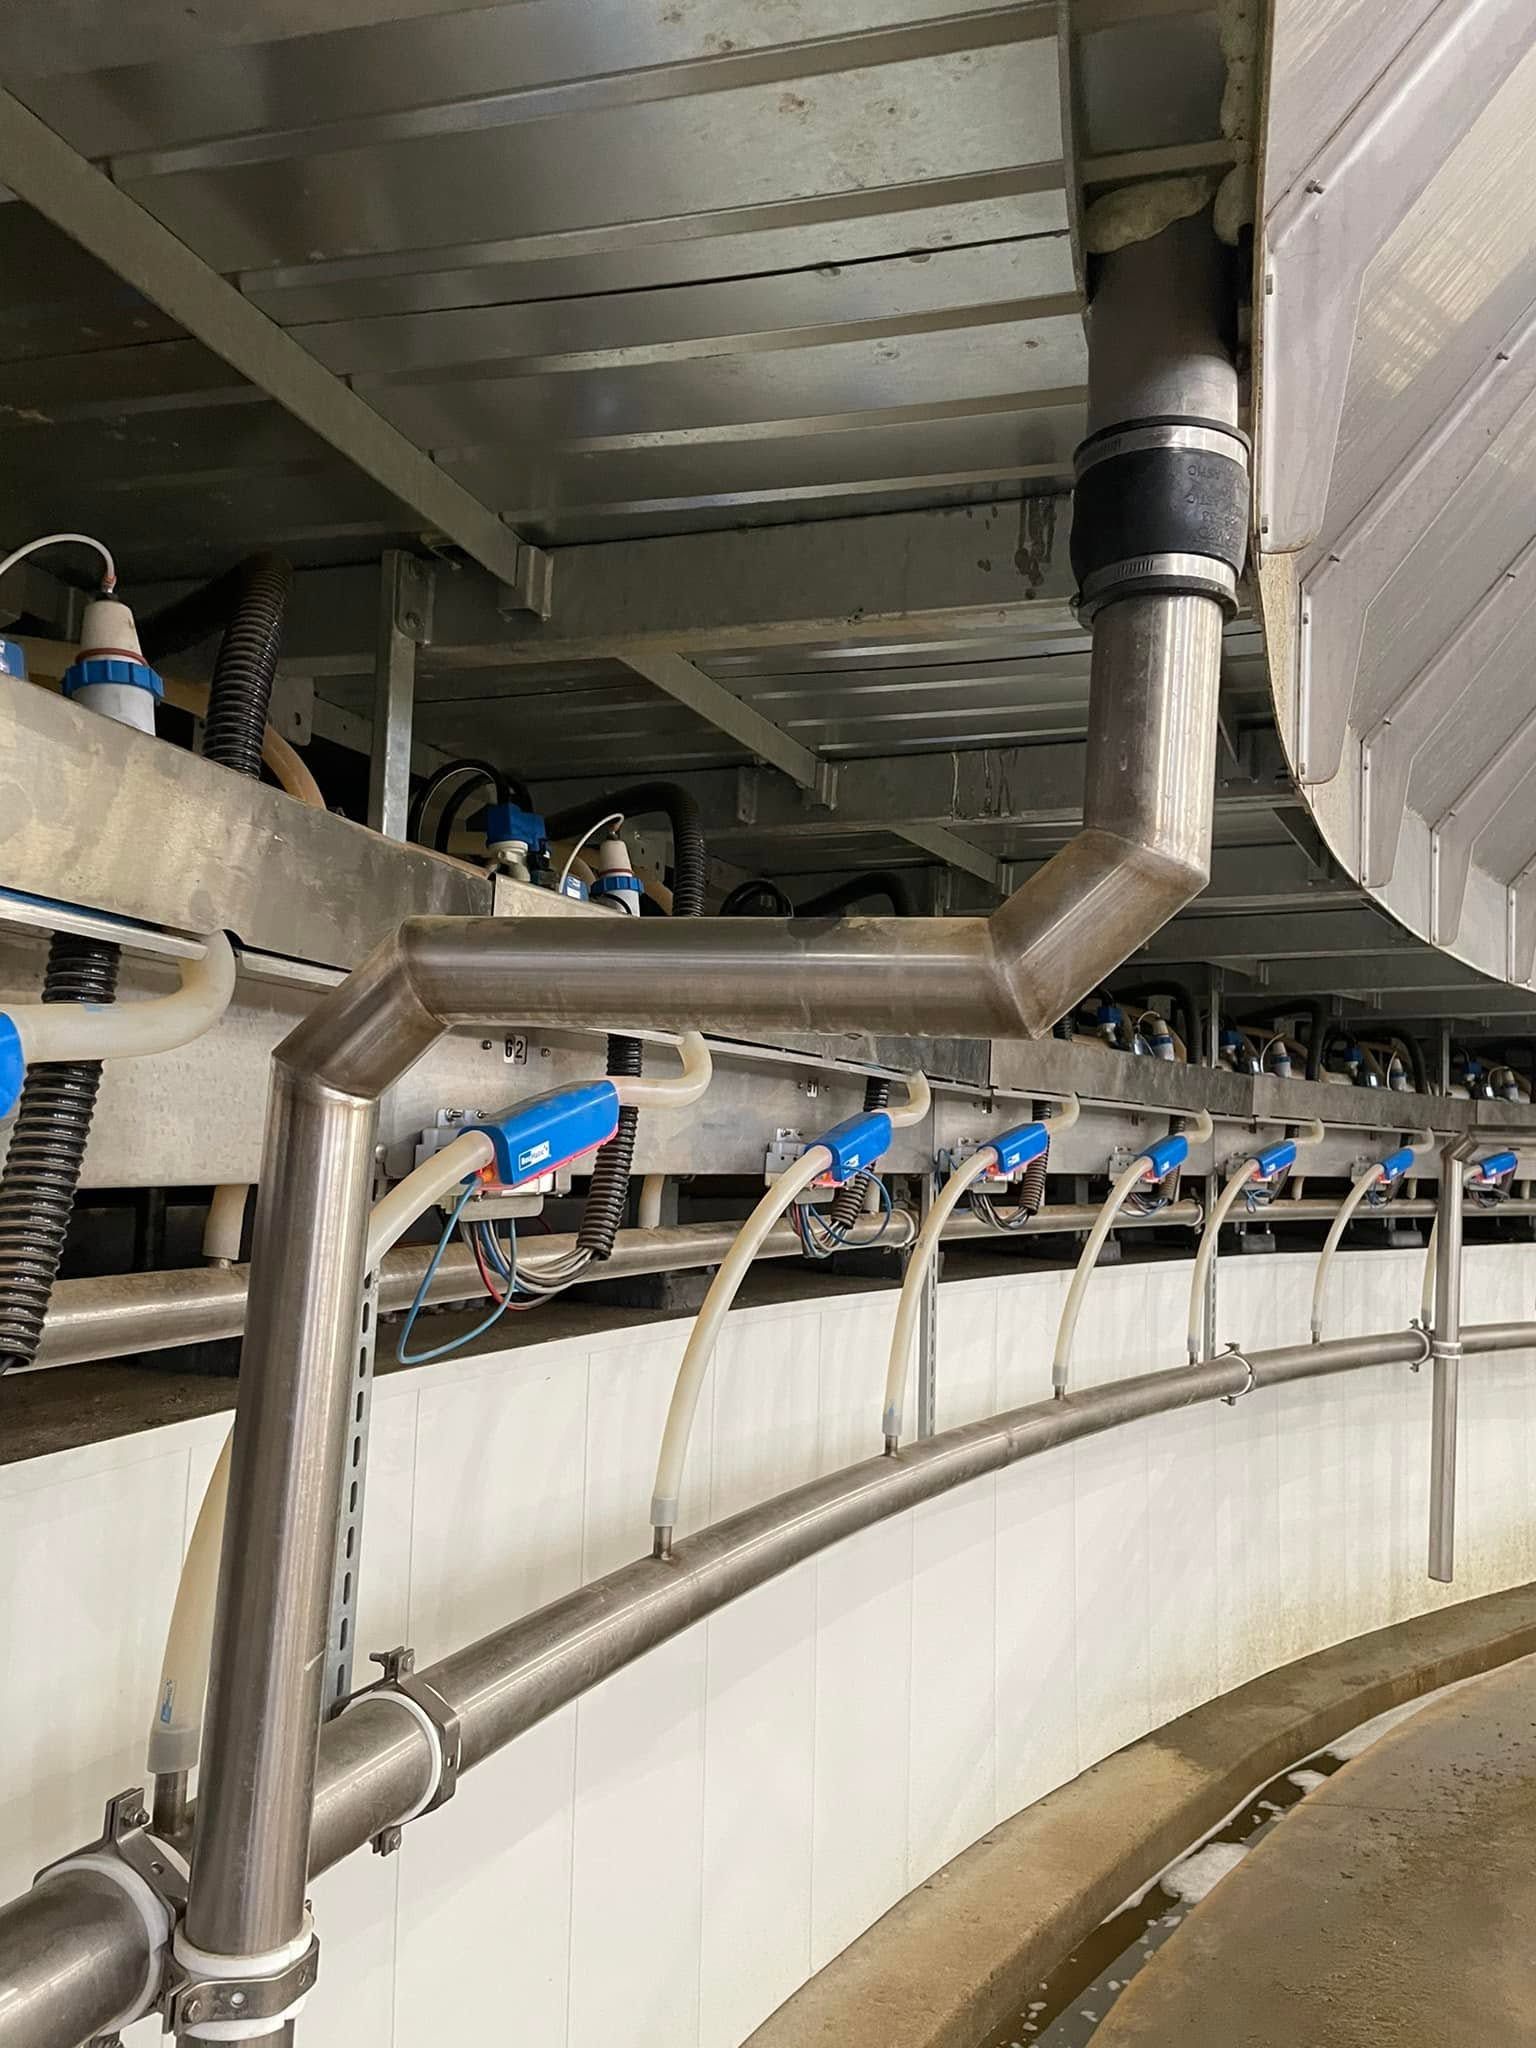
Stainless sanitary line installed in a rotary dairy parlor
Grade A dairies

Dairies

Parlor and milk-room pipelines, receivers, bulk tank fittings, wash and CIP lines, and the repairs that come up between inspections. Built so the state inspector can scope it and move on.

  • Milk lines
  • Receivers
  • Bulk tank fittings
  • CIP and wash lines
  • Parlor piping
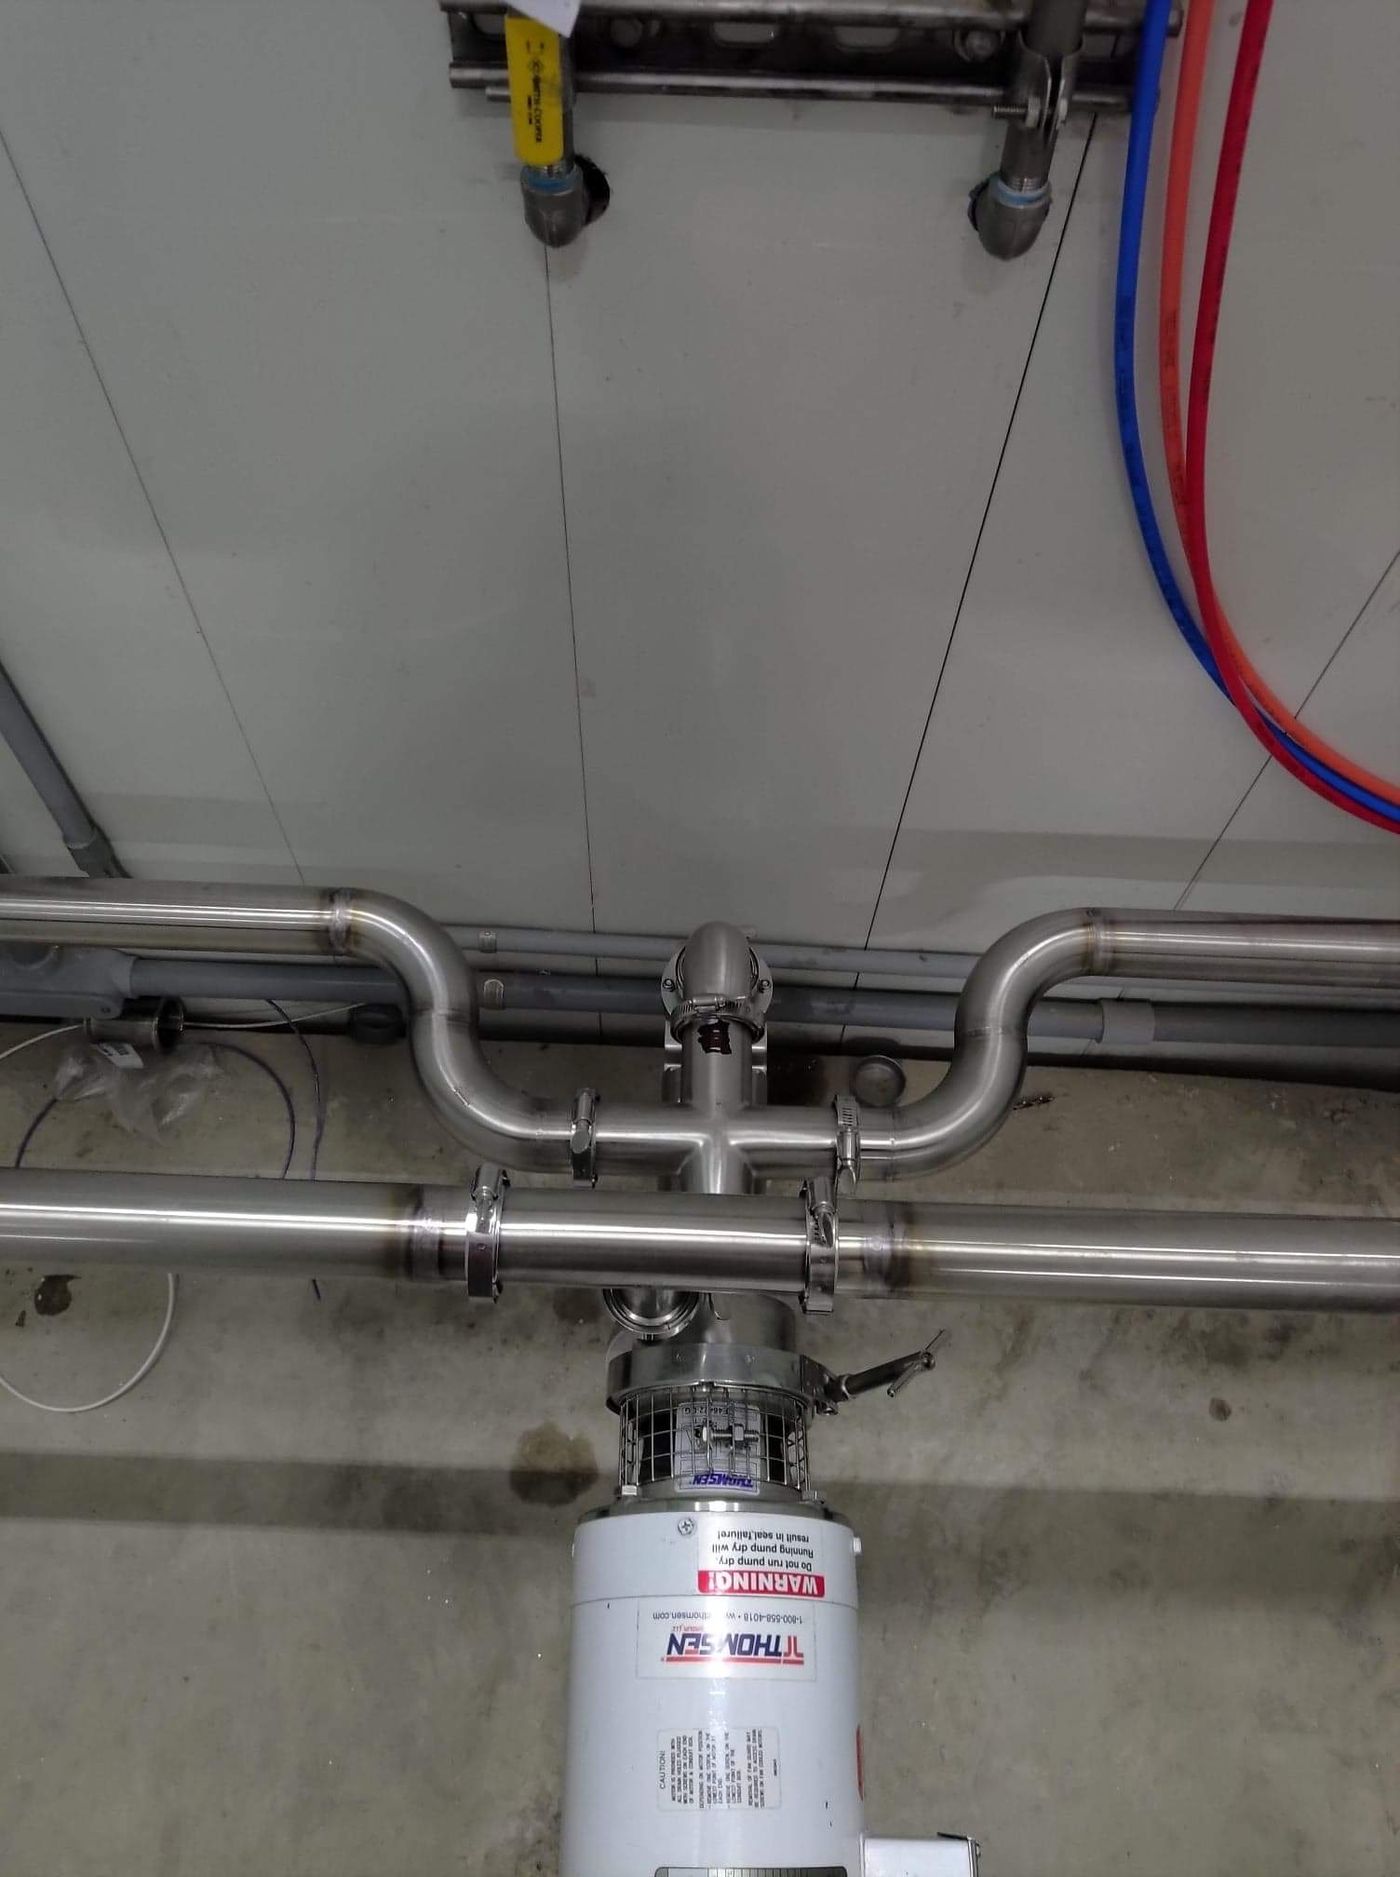
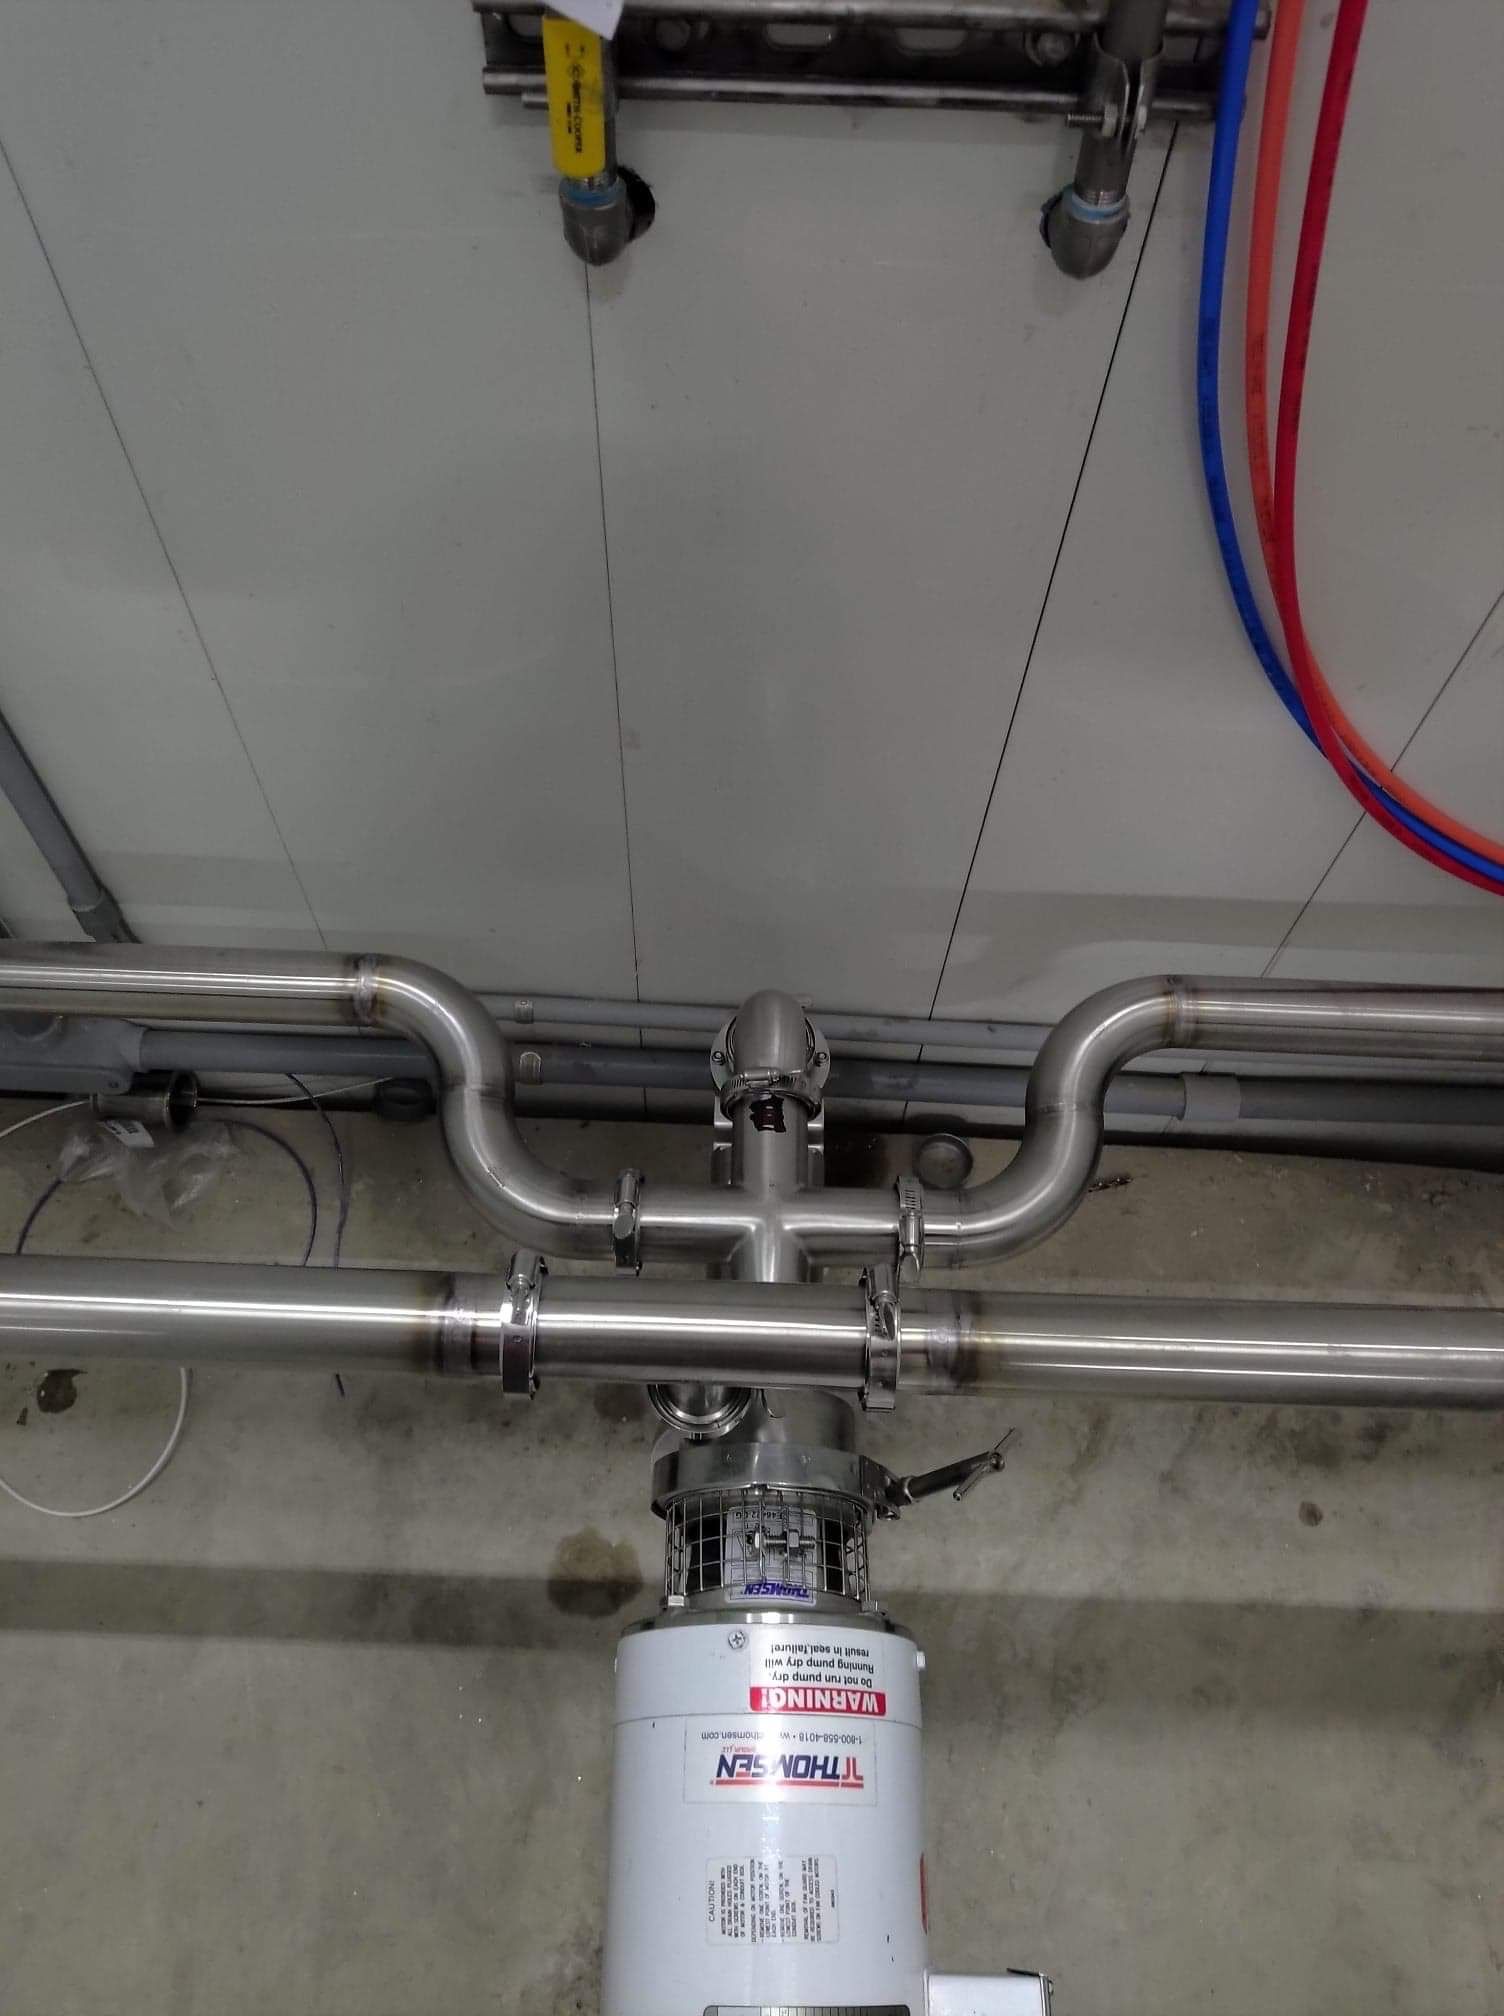
Stainless Tri-Clamp product line over a dairy pump
Craft and production

Breweries

Brewhouse and cellar piping, hard-piped transfer lines, Tri-Clamp manifolds, fermenter and brite tank ports, heat exchanger connections and CIP loops. Purged and finished so the inside of the line is as clean as the outside.

  • Transfer lines
  • Tri-Clamp manifolds
  • Tank ports
  • CIP loops
  • Heat exchanger piping
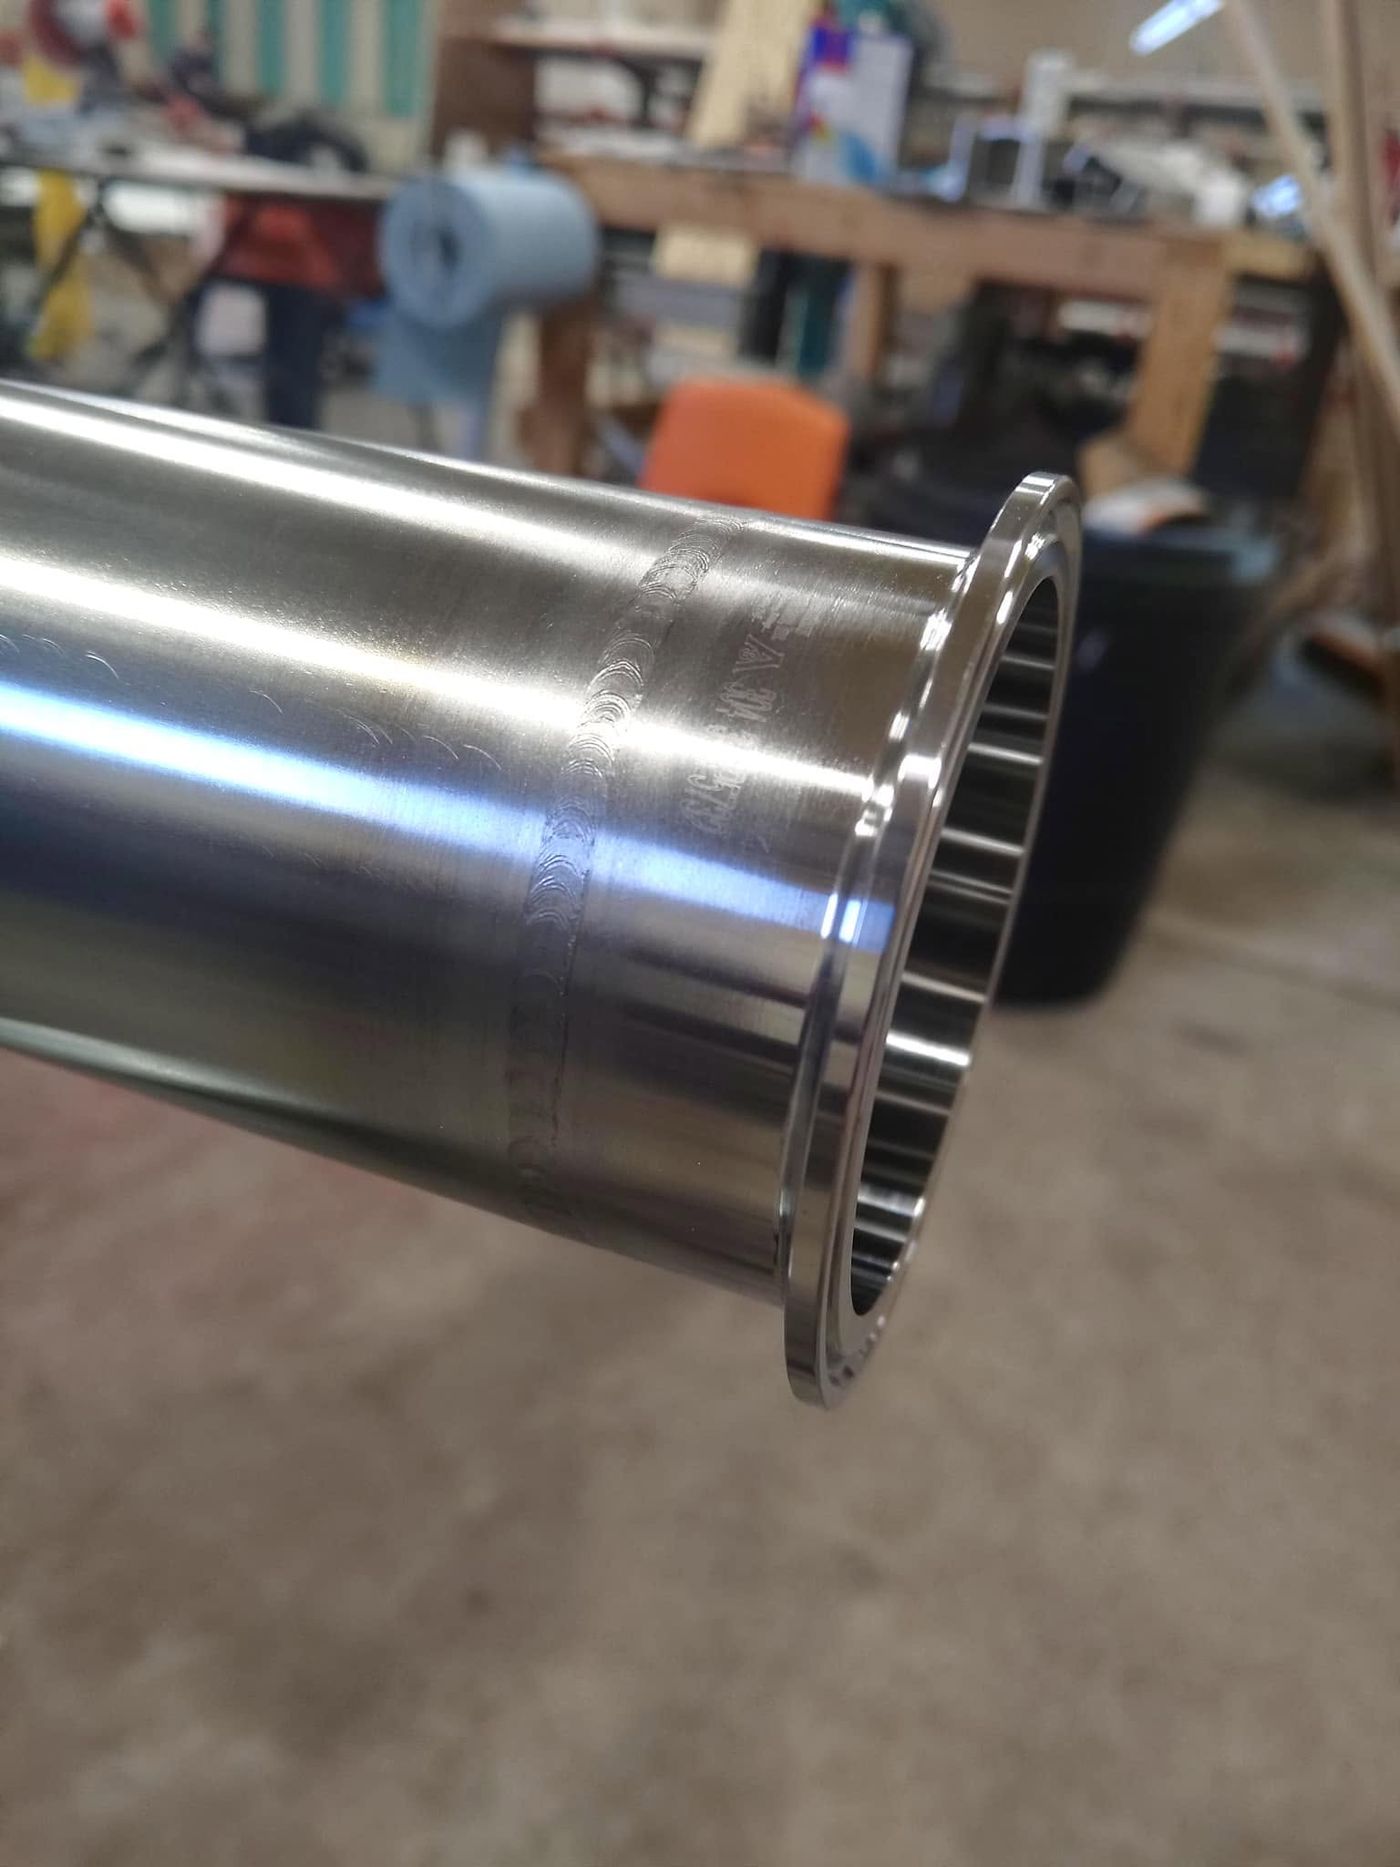
Sanitary stainless tube with a welded Tri-Clamp ferrule
Tasting room to tank room

Wineries

Tank fittings and valves, racking and transfer lines, crush pad and press piping, and replacing the fitting that cracked the week before harvest.

  • Tank fittings
  • Racking lines
  • Press piping
Spirits

Distilleries

Still and condenser connections, spirit and low-wines transfer lines, Tri-Clamp valve assemblies and custom stainless pieces. Caleb already keeps one Oregon distillery running.

  • Still connections
  • Spirit lines
  • Valve assemblies
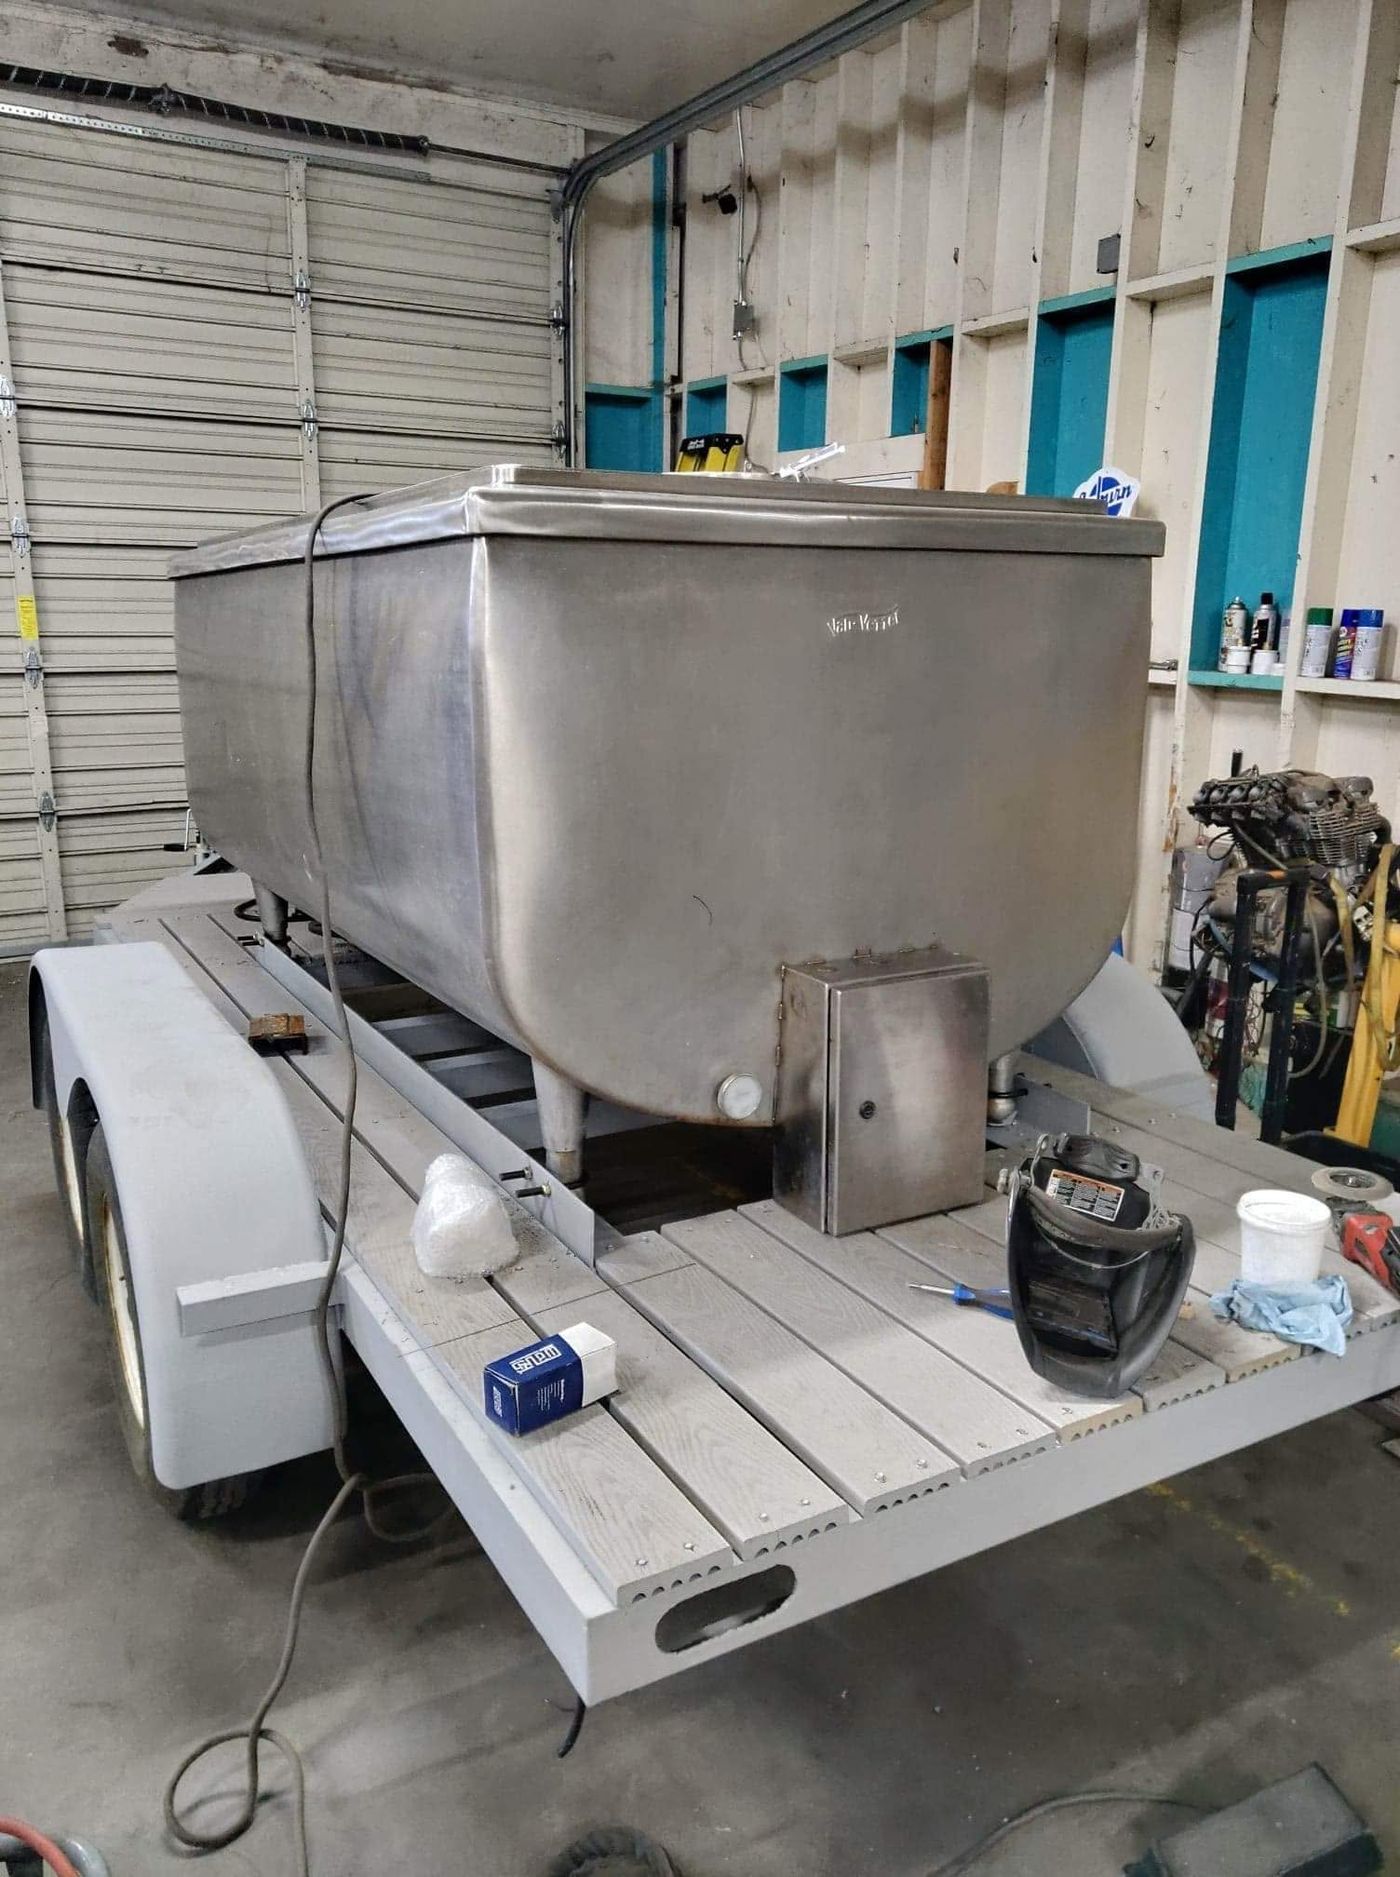
Bulk milk tank mounted on a trailer for transport
Tanks and equipment

Food-grade equipment

Bulk tanks, vessels, stainless prep and serving equipment, steam tables and the one-off stainless pieces a processor or commercial kitchen needs repaired or built.

  • Bulk tanks
  • Vessels
  • Kitchen stainless

Not sanitary, still stainless or steel? Gates, trailers, farm repair and structural work run through the main shop.

Metal fabrication
How a sanitary job runs

Four steps. No shortcuts on any of them.

Sanitary work takes longer per joint than general fabrication, and it should. Here is where that time goes.

01

Walk the line

On site or from your photos. What is failing, what the inspector flagged, what alloy and tube size you run, and how much downtime you can afford. Milking schedules and brew days set the plan.

02

Fit up

Matching 304 or 316L tube and Tri-Clamp fittings. Ends cut square, deburred, aligned flush and pitched to drain. Stainless-only tooling from the first cut.

03

Purge and weld

Argon back-purge on every product-contact joint, then full-penetration TIG at low heat so the root stays bright and the tint stays light.

04

Inspect and hand off

Every joint checked. Representative welds left unpolished for the borescope, and Caleb is available to walk your inspector through the work.

We work with your inspector, not around them.

Caleb has a working relationship with the dairy inspectors in this part of the valley and has walked several of them through what a passing sanitary weld looks like. If your inspector has a question about a joint, he will take the call. It is better for everybody when the welder and the inspector are looking for the same thing.

Start a sanitary quote
Recent sanitary work

Stainless that had to pass.

Dairy pipelines, Tri-Clamp assemblies and tank work from around the valley. Most of it is photographed before polishing, because that is the state the inspector sees it in.

Stainless sanitary pipeline installed in a rotary dairy parlor
Rotary parlor pipelineStainless milk line, dairy
Stainless Tri-Clamp product line over a dairy pump
Tri-Clamp product lineMilk room, dairy
Bulk milk tank mounted on a trailer for transport
Bulk milk tank, mountedMueller tank on a trailer
Tri-Clamp ferrule welded to sanitary stainless tube
Ferrule on sanitary tubeUnpolished for inspection

More welding and fabrication work, sanitary and otherwise, is in the project galleries.

What customers say

Shows up, does it right, sticks with it.

5.0
★★★★★16 Google reviews, every one of them five stars
★★★★★

Punctual. Efficient. Knowledgeable. Caleb does quality work. If I need TIG work again, and I probably will, I will definitely be calling him back.

Jess VGoogle
★★★★★

Professional and efficient. Great quality at a great price. Same day service. Would highly recommend.

Pete MaciasGoogle
★★★★★

Caleb is a professional welder and fabricator. I hired him for a big job for our business. He delivered, and stuck with it till it was done, which proved to be a late night. Now how many people would do that? His pricing is most fair.

Michael DowdGoogle

Reviews are from Google and are quoted as written, trimmed for length.

Questions

Straight answers on sanitary work.

If yours is not here, text a photo of the joint or the fitting and ask.

Ask about a job
What is sanitary welding?

Welding stainless steel that food, milk or beverage will touch, to a standard where the inside of the joint is as smooth and clean as the tube around it. That means argon back-purging, full penetration, controlled heat so the metal does not discolor, no pits or crevices, and lines that drain. It is governed by 3-A Sanitary Standards and AWS D18.1 and checked by dairy and food inspectors, usually with a borescope.

Are you certified for sanitary welding?

Yes. Sanitary welding has its own test, separate from structural or pipe certifications, and Caleb has taken and passed it. Certification paperwork comes with the quote on request.

Do you come to the farm or the brewery?

Yes. Most sanitary work is mobile: parlors, milk rooms, brewhouses, cellars and tank rooms across the Willamette Valley. Spools, manifolds and tank work that can travel are built in the Monmouth shop.

Will the work pass my dairy inspection?

It is built to the same criteria the inspector uses: 3-A Accepted Practice 605 and AWS D18.1. Welds are left unpolished so representative joints can be scoped, and if your inspector flags anything we rework it. Caleb will also talk directly with the inspector if that helps.

A line failed during milking. Can you come now?

Call. After-hours and emergency calls are available at an after-hours rate, and a dairy that cannot ship milk is exactly what that is for.

Why does sanitary welding cost more than regular welding?

More prep, argon purge gas on every joint, dedicated stainless-only tooling, and more time per weld. A sanitary joint takes longer than a structural one because the inside has to be perfect, not just the outside. The rate reflects that, and it is still far cheaper than a dumped tank or a lost batch.

What stainless do you work with?

304 and 316L sanitary tube and Tri-Clamp fittings, matched to what is already in your plant. 316L where acid, salt or chlorides are involved. If you are not sure what you have, send a photo of a fitting and the stamp on it.

Do you do non-sanitary stainless and steel too?

Yes. Gates, railings, trailers, farm equipment and structural repair run through the main shop. See metal fabrication and repair and maintenance.

Where we work

Based in Monmouth. Mobile across the valley.

Dairies, breweries, wineries and distilleries from McMinnville down to Lebanon, and farther for the right job. If your plant is outside this list, call and ask.

  • MonmouthHome base
  • IndependencePolk County
  • DallasPolk County
  • SalemMarion County
  • KeizerMarion County
  • WoodburnMarion County
  • CorvallisBenton County
  • AlbanyLinn County
  • LebanonLinn County
  • McMinnvilleYamhill County
  • HayesvilleMarion County
  • Four CornersMarion County
Get it done right the first time

Tell us what is failing, or what you are building.

Send a photo of the joint, the tank or the drawing. You will hear back from Caleb, not a call center, with a straight answer on whether it is a sanitary job and what it takes.

Get a sanitary quote Call (530) 385-0730

Text works best. Caleb is usually under a hood. Veteran owned, Monmouth, Oregon.